How to Choose a Transformer Production Line?
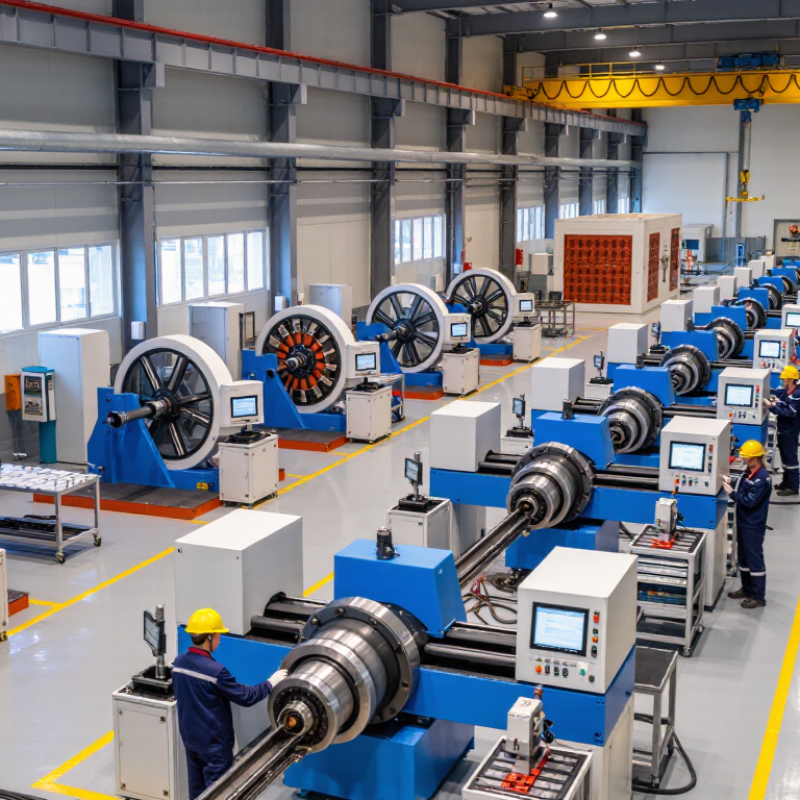
Choosing a Transformer Production Line is a practical decision with long-term consequences. It affects product quality, operating costs, worker safety, and delivery performance. A line that looks impressive in a showroom may perform differently in a real factory. Dust, humidity, unstable power, limited floor space, and changing order sizes can expose hidden weaknesses.
Experienced manufacturers usually begin with the transformer types, voltage ranges, core dimensions, and expected annual output. These details guide decisions about winding machines, core cutting systems, insulation equipment, drying ovens, assembly stations, and testing instruments. Production speed matters, but consistency matters more. A winding machine that produces uneven tension can create costly defects later. Small errors become expensive.
Ask practical questions.
Can operators maintain the equipment without waiting weeks for overseas technicians? Are replacement parts available locally? Does the supplier provide installation training, process documentation, and reliable after-sales support? Independent test reports, factory references, and performance records deserve careful review. Claims alone are not enough.
A reliable evaluation should include a factory visit, sample production, energy consumption data, noise levels, and a realistic maintenance schedule. Buyers should also compare automation with actual labor skills. Full automation may appear efficient, yet it can be unsuitable for smaller batches or frequent design changes. I have seen projects focus heavily on output capacity while underestimating commissioning time. That mistake can delay production for months.
The best Transformer Production Line is not always the fastest or most expensive. It should match technical requirements, workforce capability, quality targets, and future expansion plans. Leave room for honest uncertainty. A thoughtful decision protects investment and supports stable production.
Define Transformer Type, Rating, and Frequency Under IEC 60076
How to Choose a Transformer Production Line?
Define Transformer Type, Rating, and Frequency Under IEC 60076
Choosing a transformer production line starts with a precise product definition. IEC 60076 provides the technical framework for power transformers, including insulation, temperature rise, tests, and performance requirements. Identify the transformer type before discussing machinery. It may be oil-immersed or dry-type, single-phase or three-phase, and designed for distribution or power service. Each choice affects winding equipment, drying systems, assembly space, and testing capacity.
The rating must describe more than a single MVA value. Record rated power, high- and low-voltage levels, connection symbol, impedance, insulation level, cooling method, and permitted temperature rise. For example, a 10 MVA transformer rated at 33/11 kV needs different production controls from a smaller 400 kVA unit. Frequency is equally important. State 50 Hz or 60 Hz clearly, because frequency influences core design, flux density, losses, and verification tests. A vague frequency assumption can create expensive rework.
Match Core, Coil, and Tank Processes to 10–1,000 kVA Output
How to Choose a Transformer Production Line?
Choosing a transformer production line starts with the output range, not the machine catalog. For 10–100 kVA units, a compact core cutting line, simple winding equipment, and a manual or semi-automatic tank station may be sufficient. These transformers often use smaller conductors and lighter tanks. Operators can correct winding tension quickly. That matters. However, manual work can create unwanted variation.
From 100 to 400 kVA, specify controlled core joining, coil winding, drying, and tank fabrication. Step-lap core assembly can reduce losses when joints are accurate. Foil or wire winding should match conductor size, insulation design, and short-circuit requirements. Add tension monitoring and dimensional checks. A line may look fast on paper. It may still bottleneck during drying or testing.
For 400–1,000 kVA, production usually needs heavier handling, automated winding control, vacuum drying, and consistent tank welding. The core line should move larger laminations without damaging their edges. Coil equipment must maintain pressure and alignment across longer windings. Tank processes require leak testing, bushing positioning, surface preparation, and controlled coating.
I have seen lines optimized for winding but slowed by crane movement. Layout is production equipment too. Review daily volume, product variety, and available floor space before choosing. A perfect design rarely survives unchanged. Pilot runs reveal more than brochures.
Compare Automation Levels Using Cycle Time, OEE, and Labor Requirements
How to Choose a Transformer Production Line?
Compare Automation Levels Using Cycle Time, OEE, and Labor Requirements
Choosing a transformer production line requires more than comparing machine speeds. Cycle time shows how long one unit takes under defined conditions. Measure loading, winding, assembly, testing, and changeovers separately. A quoted cycle time may exclude material handling or inspection. Small delays accumulate.
OEE provides a more realistic view. It combines availability, performance, and quality. Record unplanned stops, reduced speeds, and rejected units during representative production runs. An automated line may produce one transformer every few minutes, yet frequent sensor faults can reduce availability. Manual lines can appear slower, but skilled workers may recover from product variations more quickly. The comparison must use the same product mix and shift length.
Labor requirements also change with automation level. Count operators, material handlers, inspectors, technicians, and supervisors. Semi-automated equipment may need more hands-on work, but it can simplify maintenance and changeovers. Highly automated equipment often reduces direct labor while increasing programming and troubleshooting demands. Training time matters. So does ergonomic risk.
Use measured data rather than sales estimates. Pilot testing helps. My experience suggests that early calculations often overlook rework and waiting time. That is worth challenging. A line with excellent theoretical speed may perform poorly when copper sizes, insulation designs, or order quantities change. Leave practical space for maintenance access, operator movement, and future product adjustments.
How to Choose a Transformer Production Line? - Compare Automation Levels Using Cycle Time, OEE, and Labor Requirements
| Production Line Type | Typical Manufacturing Scope | Nominal Cycle Time (min/unit) | Expected OEE | Direct Labor (operators/shift) | Estimated Output (units/shift) | Changeover Time (min) | Best-Fit Production Profile |
|---|---|---|---|---|---|---|---|
| Manual | Coil preparation, winding, core assembly, connection, and inspection performed mainly by operators | 45–70 | 45–60% | 12–20 | 5–8 | 30–60 | Low-volume production, frequent product variation, and limited initial capital |
| Semi-Automated | Automated winding or cutting combined with manual loading, assembly, testing, and material handling | 25–45 | 55–70% | 8–14 | 8–14 | 20–40 | Medium-volume production with several transformer ratings and moderate customization |
| Highly Automated | Integrated winding, taping, cutting, transfer, assembly support, testing, and production tracking | 12–25 | 65–80% | 4–8 | 14–28 | 15–30 | Stable product families, repeatable demand, and a strong need to reduce labor per unit |
| Advanced Flexible | Automated material flow, programmable processing, inline inspection, digital traceability, and robotic handling | 8–18 | 70–85% | 3–6 | 20–40 | 10–20 | High-volume production requiring consistent quality, traceability, and rapid recipe changes |
Verify 50/60 Hz Testing, 2–2,500 kV Impulse, and IEC 60076 Compliance
How to Choose a Transformer Production Line?
A credible production line must prove its dielectric testing range, not merely advertise it. Verify 50 Hz and 60 Hz testing with calibrated voltage and frequency records. The test bay should support impulse levels from 2 kV to 2,500 kV, matching the transformer design and insulation class. IEC 60076-3:2013+A1:2018 defines insulation, dielectric, and impulse-test requirements for power transformers. Ask for recent test certificates, calibration dates, and waveform records. Paperwork matters.
Impulse testing needs more than a powerful generator. Check the measuring divider, grounding layout, control system, and response time. A clean impulse trace should show repeatable front time, peak voltage, and oscillation control.
CIGRE Technical Brochure 642, Transformer Reliability Survey, identifies windings, insulation systems, and bushings as recurring transformer failure areas. That evidence makes impulse and applied-voltage testing practical risk controls, not decorative specifications.
Frequency testing also deserves a physical check. Watch the transformer during a 50/60 Hz test: listen for abnormal vibration, inspect temperature rise, and record partial-discharge behavior where required. IEC 60076-1 and IEC 60076-3 should appear in the line’s quality documents. Do not accept a claimed 2,500 kV capability without matching test-object dimensions and safety clearances. I would also question a perfect factory demonstration. Real production includes setup errors, sensor drift, and retesting. A reliable line exposes those weaknesses before shipment.
Select Line Capacity, Quality Controls, and ISO 9001 Traceability Features
How to Choose a Transformer Production Line?
A suitable transformer production line should match output volume, product range, and inspection discipline. Capacity is not only a daily unit number. It also includes core cutting speed, winding stations, drying time, assembly space, and testing queues. The U.S. Department of Energy reported that about 70% of distribution transformers were at least 25 years old. This aging infrastructure increases demand for dependable replacement equipment and consistent production quality.
Quality controls must be visible at each critical stage. A line should record conductor dimensions, winding tension, insulation materials, torque values, vacuum pressure, and oil test results. Factory acceptance tests should cover ratio, resistance, losses, insulation strength, and partial discharge where required. ISO Survey 2023 recorded more than 1.2 million ISO 9001 certificates worldwide. Certification alone proves little, however. A rushed checklist can still hide a weak process.
Tips: Ask for sample production records, not only brochures. Check whether each serial number links to material batches, operators, calibration dates, test results, and approved corrections. Use barcode scanning at winding and assembly stations. Keep electronic records with controlled access. A paper backup is useful, but paper systems are easy to misplace. During a factory visit, follow one transformer from steel receipt to final test. If operators cannot explain a failed result, stop and investigate. Capacity claims deserve skepticism. Wider production lines may create more defects when training and inspection lag behind.
Article Source:
Get in touch with us,
We will contact you shortly!
What is the difference between Unline(Non-Epoxy Coated) or Lining(Epoxy Coated) Metal Drum?

Unline drums with internally bare metal surface is more susceptible to corrosion and rust while Lining drums are internally coated with Phenolic Epoxy Coating to provide a non-reactive barrier between the drum surface and your product, less risk of contamination. Note: Our Unline drums are coated with an anti-rust agent after washing to reduce risk of rust.
What are Unline(Non-Epoxy Coated) and Lining(Epoxy Coated) drums compatible with?

In Singapore, Recon Unline Drums are usually more costly than Recon Lining Drums. Hence, we recommend Recon Unline Drums to fill aromatics like Thinner, Xylene, Toulene& other solvents like Hexane, BA, CA, EA, MC, White spirit, etc.
We recommend the lower-priced Recon Lining Drums to fill hydrocarbons like IPA, Methanol, Ethanoland oil-based products like diesel, petrol, lubricants, engine, hydraulic, base, transmission fluid, additives, waste oil, etc.;
What is the difference between Grade A and Grade B Metal Drum ?

Grading of used drums are usually based on physical conditions like rustiness, deformities and residual contents. Grade A drums are totally free from internal rust, serious dents and are easy to clean. Grade B drums have different degrees of rust internally and aesthetically inferior compared to Grade A drums.
What content is suitable to fill in a Recon Grade A or Grade B Drum?

Recon Grade A drum is suitable to fill more costly virgin grade products while Recon Grade B drum is more suitable for recycled or waste products.
What is the difference between Open Top and Close Top Drums and their usage?

Closed top drums are for water and other liquid products. Open Top drums can be used for liquid too but are primarily for more viscous products. The Open Top (or open head with a lid) allows you to get in and out of the drum with your product easier.
What type of content are Metal or Plastic Drums suitable for?

Metal drums offer additional protection when dealing with potentially flammable substances. They provide superior fire resistance, impact protection, and longevity for storing class 1, 2, and 3 volatile chemicals.
Plastic HDPE Drums are suitable for corrosive chemicals like acids, alkaline and also water-based products.
Will there be any contamination in the reconditioned metal, plastic drums or IBC tanks?

All our reconditioned containers (metal/plastic drums, carboys, IBC tanks) are washed thoroughly with specially formulated cleaning agent, rinsed with clean water, dried, and tested for possible leakages during the recondition process. Stringent quality inspection is being conducted 100% on every reconditioned product before they are qualified for sale & delivery.
What is the drum gauge(thickness) and weight for reconditioned metal drums?

Reconditioned metal drums gauge can be 0.9mm to 1.0mm all round. Their weight can vary from 16 to 18kg.
Do you sell New Packaging Products too?

Yes, we are also a distributor for new pallets, metal drums, plastic drums, carboys, IBCs and stainless-steel tanks.
What additional services do you provide apart from selling reconditioned and new containers.?

We are an NEA licensed toxic industrial waste collector, who can collect and dispose of used toxic waste containers in Singapore.
Do you offer labelling and silkscreen on the containers ?

We can provide labelling and silk-screening on the containers.
Are you able to ship overseas ?

Yes, we can arrange export our products to any country in the world.
Leading the Way
to Carbon Neutrality