How to Choose Flue Gas Desulfurization Equipment in 2026?
Choosing Flue Gas Desulfurization Equipment in 2026 requires more than comparing removal efficiencies on product brochures. Plant operators must examine fuel sulfur content, boiler load changes, gas temperature, moisture, available land, wastewater capacity, and maintenance access. A system that performs well at steady load may struggle during frequent starts, low-load operation, or sudden fuel changes. Real operating conditions matter.
Dr. Larry L. Sloss, a recognized clean-coal and emissions-control researcher, expressed a practical principle: “No single desulfurization solution fits every plant.” That warning remains relevant. Wet limestone systems may suit large stations with reliable water and reagent supplies. Dry or semi-dry systems may better match smaller facilities with limited water availability. Seawater systems can reduce reagent handling, but coastal conditions and discharge management require careful review.
The selection process should connect engineering data with field experience. Ask how the absorber handles scaling. Check pump redundancy. Inspect access around mist eliminators and slurry lines. Review measured performance from comparable plants, not only laboratory results. A low purchase price can become expensive when corrosion, downtime, or waste treatment is underestimated.
There is no perfect choice.
Even experienced teams can miss hidden constraints. A preliminary design may look convincing, then fail during winter operation or rapid load changes. Therefore, this guide compares process chemistry, energy demand, water use, maintenance needs, lifecycle cost, and supplier support. The goal is not to promote one technology. It is to identify the most dependable Flue Gas Desulfurization Equipment for each plant’s actual conditions.
Understanding Flue Gas Desulfurization Equipment and Its Role
How to Choose Flue Gas Desulfurization Equipment in 2026?
Understanding Flue Gas Desulfurization Equipment and Its Role
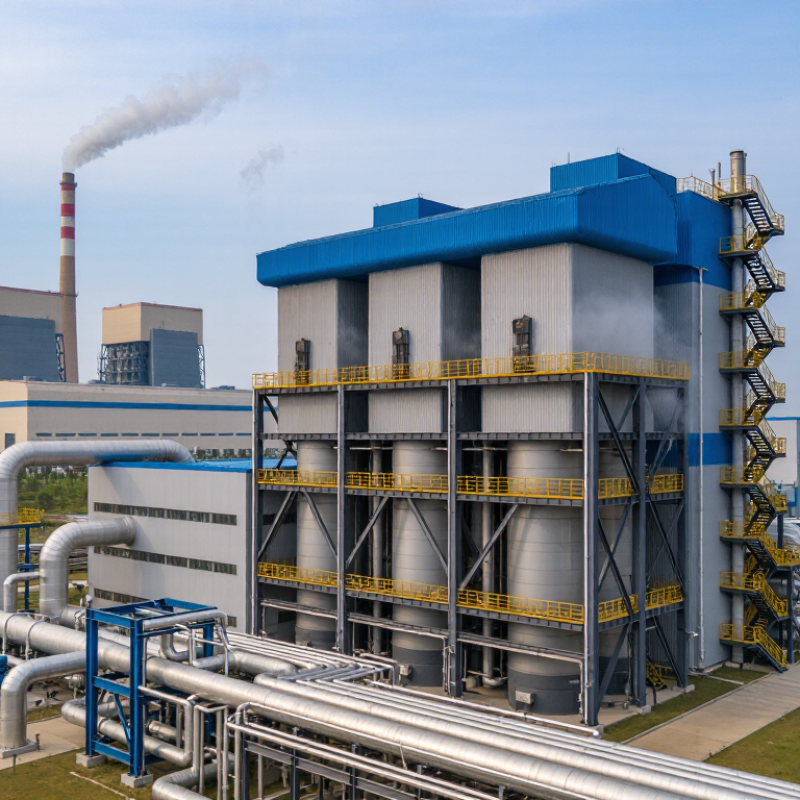
Flue gas desulfurization equipment removes sulfur dioxide from combustion exhaust. Its role is practical: protect air quality, equipment, and plant reliability. In daily operation, the system must handle changing fuel sulfur levels, gas volume, temperature, and moisture.
Wet limestone scrubbers suit large facilities with steady water access. They can achieve strong sulfur dioxide removal and produce usable gypsum. Dry and semi-dry systems may fit sites with limited water or smaller footprints. Their sorbent handling systems need careful control. Poor feeding can create uneven removal and higher operating costs.
Selection should begin with measured operating data, not sales claims. Review gas chemistry, pressure loss, chloride levels, and expected load changes. Inspectors should also consider corrosion-resistant materials around the absorber and ductwork. Online analyzers, pH sensors, and pressure monitoring support dependable control. Small sensor errors can become large compliance risks.
Maintenance experience often reveals the real equipment quality. Check access doors, spray nozzles, pumps, agitators, and slurry lines before purchase. Ask how quickly worn parts can be replaced. A system that performs well in testing may still disappoint during partial-load operation. This is often overlooked. Water treatment and byproduct management also affect total cost. A cheaper installation can create expensive wastewater problems later.
No design is perfect. Engineers must balance removal efficiency, water use, energy demand, maintenance, and local conditions. Pilot testing can expose issues that calculations miss. Reliable selection combines verified data, operator feedback, independent inspection, and realistic lifecycle costing.
How to Choose Flue Gas Desulfurization Equipment in 2026? - Understanding Flue Gas Desulfurization Equipment and Its Role
Comparison of major flue gas desulfurization technologies and the key technical factors used when selecting equipment for industrial and power-generation applications.
| Technology | Typical SO₂ Removal Efficiency | Typical Applications | Water Demand | Main By-Product | Key Advantages | Main Limitations |
| Wet Limestone Scrubbing | 90–99% | Large coal-fired power plants, industrial boilers, and high-sulfur fuel applications | High; requires slurry preparation and wastewater management | Gypsum slurry or gypsum by-product | Highest removal potential, mature process, suitable for strict emission limits | Large footprint, corrosion control requirements, pumps and slurry-handling equipment |
| Spray Dry Absorption | 80–95% | Medium-sized boilers and facilities requiring lower water use than wet systems | Moderate; water is atomized and largely evaporates in the absorber | Dry calcium sulfite/sulfate-rich residue | Lower wastewater generation, relatively compact layout, dry solids handling | Higher reagent consumption and generally lower maximum removal than wet scrubbing |
| Dry Sorbent Injection | 40–80%, depending on sorbent, temperature, residence time, and flue-gas conditions | Smaller industrial boilers, process heaters, and retrofit projects with limited space | Very low or none | Spent sorbent mixed with captured fly ash | Simple installation, low capital cost, small footprint, fast response to load changes | Higher solid waste volume and limited suitability for very stringent SO₂ limits |
| Circulating Dry Scrubber | 85–95% | Medium and large combustion units where dry operation and high removal are required | Low to moderate | Dry calcium-based reaction product | High removal efficiency without liquid effluent, lower water use than wet systems | Requires reliable solids recirculation, baghouse capacity, and precise process control |
| Seawater Flue Gas Desulfurization | 90–98% | Coastal power stations and facilities with suitable seawater availability | Uses seawater; no limestone slurry system is required | Treated seawater containing oxidized sulfur compounds | No limestone handling, no gypsum disposal, and relatively simple reagent logistics | Requires suitable coastal conditions, marine discharge controls, and careful corrosion management |
| Selection Criterion | What to Evaluate | Why It Matters in 2026 |
| Required Emission Limit | Permitted SO₂ concentration, mass emission rate, averaging period, and startup or low-load requirements | The required limit determines whether a high-efficiency wet or dry system is necessary. |
| Flue-Gas Conditions | Gas flow, temperature, moisture, oxygen content, particulate loading, and inlet SO₂ concentration | These variables affect absorber sizing, reagent reaction, corrosion risk, and removal efficiency. |
| Fuel Sulfur Content | Average and maximum sulfur content, fuel switching frequency, and expected load profile | Higher sulfur input increases reagent demand, residue production, and equipment capacity requirements. |
| Water Availability | Freshwater supply, wastewater discharge limits, water recycling capability, and local climate | Water scarcity or strict discharge requirements may favor dry or semi-dry technologies. |
| Space and Retrofit Constraints | Available plot area, duct routing, structural load limits, outage duration, and tie-in points | Compact systems and modular equipment can reduce construction work at existing facilities. |
| Lifecycle Cost | Capital cost, reagent consumption, electricity use, water use, maintenance, residue disposal, and downtime | The lowest purchase price may not provide the lowest total cost over the equipment lifetime. |
| By-Product Management | Potential for gypsum use, residue storage, ash compatibility, disposal routes, and product quality | A usable by-product can reduce disposal costs, while contaminated residue may require controlled handling. |
| Automation and Monitoring | Continuous SO₂ monitoring, pH or reagent control, differential pressure, temperature, flow, and alarm systems | Advanced monitoring supports stable compliance, predictive maintenance, and more efficient reagent use. |
Note: Actual performance depends on fuel composition, inlet sulfur dioxide concentration, gas flow, absorber design, reagent quality, operating temperature, residence time, and applicable environmental regulations.
Assessing Emission Sources, Gas Conditions, and Sulfur Removal Targets
How to Choose Flue Gas Desulfurization Equipment in 2026?
Equipment selection should begin with the emission source, not a catalog. Coal, heavy fuel oil, and waste-derived fuels produce different sulfur loads. The US EPA’s AP-42 emission factors show that fuel sulfur content strongly affects SO2 generation. Measure fuel sulfur, gas flow, temperature, oxygen, moisture, and dust before sizing an absorber. A single average value can mislead.
Gas conditions determine process stability. Wet limestone systems often achieve 95–99% SO2 removal, while dry and semi-dry systems commonly reach about 85–95%, according to the EU Joint Research Centre’s Large Combustion Plants BREF. These figures are useful, not guaranteed. Chlorides, fluctuating loads, and poor atomization can reduce performance. The removal target must also reflect the applicable permit and future tightening. The US EPA’s 2023 National Emissions Inventory reported major SO2 reductions from power generation, increasing pressure for reliable compliance. Design for peak sulfur, not yesterday’s fuel.
Tips: Request at least seven days of representative gas data. Check absorber residence time and slurry oxidation capacity. Verify mist eliminator performance at low load. Ask for tested turndown data. Do not accept a perfect guarantee without operating assumptions. This is where many specifications become vague. Recheck corrosion allowances, wastewater volume, and by-product quality. A cheaper system may need more maintenance than expected.
Selecting Materials, Capacity, Energy Use, and By-Product Handling
Choosing flue gas desulfurization equipment in 2026 starts with the gas, not the catalog. An experienced engineer reviews sulfur levels, chloride concentration, temperature swings, dust loading, and oxygen content. These details determine whether lined steel, corrosion-resistant alloys, or engineered polymers can survive continuous service. Material choice is never decorative. Inspectors should compare corrosion coupons, weld quality, abrasion zones, and access for future repairs. One overlooked chloride spike can shorten an absorber’s service life.
Capacity must match real operating patterns, not only the nameplate load. Engineers should examine minimum, normal, peak, and future flue gas volumes. An oversized system may waste pumping power and dilute operating control. An undersized system may struggle during fuel changes or seasonal demand. I have seen planning models look precise while missing frequent load swings. That weakness deserves attention. Fan pressure drop, slurry circulation, oxidation air, and pump efficiency strongly influence energy use. Variable-speed drives can reduce consumption during low-load operation, but their benefits depend on stable controls and proper maintenance.
By-product handling should be designed beside the absorber, not added later. The assessment should cover gypsum quality, dewatering performance, storage space, dust control, wastewater treatment, and transport access. If the by-product contains excessive impurities, reuse may become impractical. A simple disposal assumption can hide major costs. Pilot testing with representative fuel and water is often more reliable than laboratory data alone. Operators should also record moisture, particle size, and chloride levels during commissioning, because real conditions rarely behave perfectly.
How to Choose Flue Gas Desulfurization Equipment in 2026?
Typical SO₂ removal performance by FGD technology
Selection guidance: Wet limestone systems generally provide the highest SO₂ removal and produce gypsum that can often be dewatered for beneficial use. Spray-dry absorbers typically require less water and are suitable for medium-capacity units, while dry sorbent injection has lower installation complexity but usually offers lower removal efficiency and higher reagent consumption.
Final equipment selection should also consider flue-gas volume, chloride and corrosion exposure, absorber materials, electrical power demand, water availability, reagent logistics, and the required handling or disposal route for solid by-products. The values shown are representative engineering ranges summarized as typical midpoints; actual performance depends on coal or fuel sulfur content, inlet conditions, reagent quality, and operating control.