China Top Shuttering Magnet Manufacturers and Suppliers
Shuttering Magnet systems help secure formwork during precast concrete production, reducing the need for drilling or welding on steel casting beds. Their compact housings contain powerful magnets, while a push-button or lever mechanism releases them when panels need repositioning. On a busy factory floor, that can mean faster setup, cleaner bed surfaces, and fewer interruptions. Small details matter.
China has a broad network of shuttering magnet manufacturers and suppliers serving precast plants, mold makers, and equipment distributors. Yet a catalog photo cannot reveal everything. Buyers should compare holding force, dimensions, casing durability, release mechanism, and compatibility with their formwork. Ask for product drawings, test information, customization options, and clear answers about packaging and lead times. A supplier’s response to practical questions can be as informative as its product list.
This guide introduces factors for evaluating China-based suppliers and choosing a Shuttering Magnet for real production conditions. It also highlights the value of checking quality-control procedures, communication, and after-sales support before placing an order. Specifications deserve careful review. A magnet that performs well in one setup may not suit another, especially when panel weight, bed condition, or operating habits differ. No shortlist can replace a proper technical assessment, and supplier claims should be verified. That extra step may feel slow, but it can prevent costly mismatches later.
Shuttering Magnets Explained: Magnetic Circuits, Components, and Precast Uses
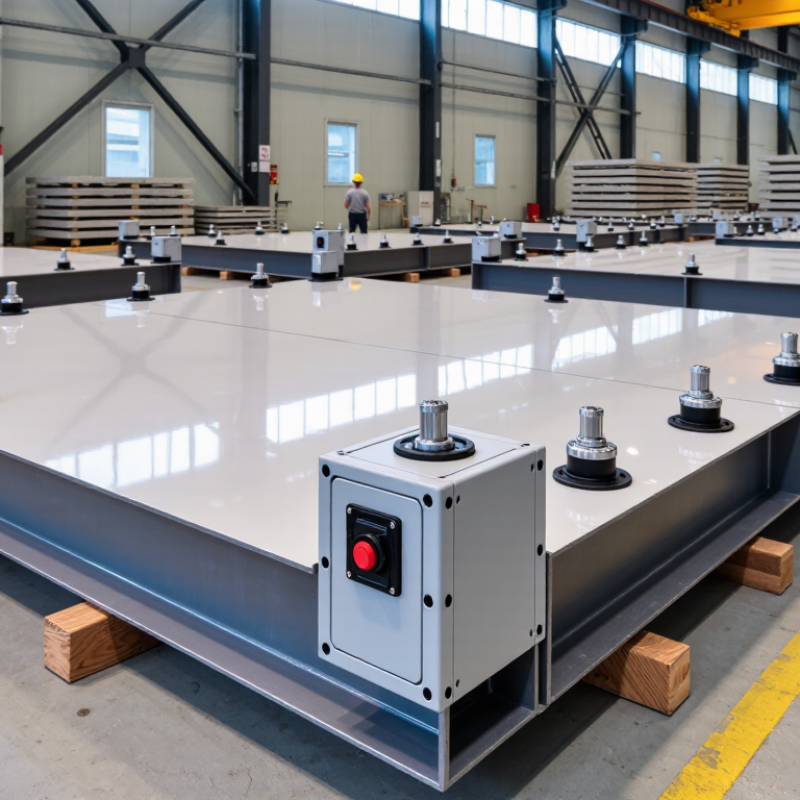
Shuttering magnets hold formwork against a steel casting bed without drilling or clamping through the table. Their magnetic circuit typically combines permanent magnets, a steel casing, and a switching mechanism. When activated, magnetic flux travels through the casing and into the steel bed, creating the holding force. A lever or release tool changes the magnet’s state, so crews can reposition forms between pours. Small parts matter. Concrete paste, rust, or a thin air gap can reduce contact and weaken the hold.
The application is growing alongside precast production. Grand View Research’s Precast Concrete Market report values the global market at USD 130.4 billion in 2023. It forecasts 6.7% annual growth through 2030. That market figure does not measure magnet demand directly, but it signals wider use of factory-made concrete elements. On a casting bed, magnets help secure side rails and block-outs while keeping the table surface intact. Yet rated holding force is not a complete safety measure. Check bed condition, magnet placement, and formwork loads before pouring. Even experienced crews can miss a small gap. That deserves a second look.
Key Selection Data: Holding Force, Contact Area, and 24 kN/m³ Concrete Density
China Top Shuttering Magnet Manufacturers and Suppliers
Key Selection Data: Holding Force, Contact Area, and 24 kN/m³ Concrete Density
When comparing shuttering magnet manufacturers and suppliers, check how holding force was measured. A published rating usually assumes clean, flat steel and ideal contact. Real formwork may have paint, weld marks, or slight warping. These reduce effective contact and can weaken retention. Small gaps matter. Select magnets with a suitable safety margin for the panel and pour conditions, rather than relying on the headline force alone.
Contact area affects how force transfers into the formwork. A larger footprint can distribute load more evenly, but only when the whole face sits flush. For fresh concrete, use 24 kN/m³ as a practical unit weight in preliminary pressure estimates. At one metre of concrete depth, a simple hydrostatic estimate is about 24 kPa. Actual pressure also depends on pour rate, temperature, vibration, and mix behavior, so this figure is not a complete design check.
Tips: Before pouring, clean the magnet and steel surface, seat the unit firmly, and inspect the panel for movement. Confirm the supplier’s test conditions and check whether its rating applies to the full contact face. Field results can differ from the catalogue; record any slipping or uneven seating and reassess the setup before the next pour.
China Shuttering Magnet Selection: Holding Load, Contact Area & Fresh Concrete Density
Illustrative static-pressure calculations for fresh concrete at a density of 24 kN/m³. The chart shows pressure at the stated depth and the resulting lateral load on one metre of formwork.
Assumption: fresh concrete behaves hydrostatically, so pressure is p = ρgh and the resultant load per metre of formwork is F = ½ρgh². These are calculated loads, not magnet ratings. For selection, distribute the design load across the magnets, apply appropriate safety factors, and verify each magnet’s rated holding force and effective contact area against the actual formwork surface and installation conditions.
Quality Verification: Pull-Force Testing, Surface Protection, and ISO 9001:2015
For shuttering magnet manufacturers and suppliers, pull-force figures need context. A high number on a product sheet is not enough. Ask how the magnet was tested: on what steel thickness, with what surface condition, and in which direction was force applied? A calibrated force gauge and a clean, flat steel plate make comparisons more meaningful. Record the test setup, not just the result. Small details matter.
During a factory visit or sample inspection, look for stable contact between the magnet and formwork. Dust, a slight air gap, or uneven steel can reduce holding force. Results may vary between test rigs; that is worth acknowledging, not hiding. Surface protection deserves equal attention. Check coating coverage around edges, corners, and switch openings, where chips often start. After repeated use, inspect for scratches, rust, concrete residue, and loose parts. A protective finish helps, but it cannot prevent damage caused by rough handling.
ISO 9001:2015 indicates a quality management system, not a guarantee that every magnet meets a particular pull-force target. Ask suppliers for inspection records, batch traceability, and documented corrective actions when tests fail. Then compare those records with samples from actual production. One imperfect report may reveal more than a polished brochure. Reliable verification joins measured performance with visible workmanship and repeatable process controls.
China Top Shuttering Magnet Manufacturers and Suppliers - Quality Verification: Pull-Force Testing, Surface Protection, and ISO 9001:2015
| Verification Area | Test or Review Method | Acceptance Basis | Records to Request |
|---|---|---|---|
| Pull-force performance | Measure the force required to separate the magnet from a specified, clean steel test plate using a calibrated force gauge or test machine. Record the test setup and loading direction. | Compare results with the supplier’s declared rating and agreed specification. There is no single universal pull-force value for all shuttering magnets; results depend on factors such as steel plate thickness, contact condition, air gap, and test direction. | Test report showing sample identification, plate material and thickness, contact condition, test direction, measured force, equipment identification, and calibration status. |
| Repeatability and sampling | Test multiple samples from the production lot using the same documented fixture and procedure; report individual readings rather than only a single maximum. | Use the agreed sampling plan and acceptance limits. The supplier should identify any variation from the declared rating and explain the disposition of nonconforming results. | Lot number, sample count, individual readings, acceptance criteria, inspection date, and nonconformance records where applicable. |
| Surface protection and finish | Visually inspect the housing and exposed surfaces for coating damage, corrosion, dents, sharp burrs, and contamination. Measure coating thickness when required by the purchase specification. | Meet the agreed coating type, thickness, and appearance requirements. Surfaces should have no unacceptable damage or corrosion that could affect handling, operation, or service life; numerical limits should be defined in the drawing or purchase specification. | Inspection checklist, coating specification, thickness readings when applicable, and dated photographs of sampled units. |
| Operation and release mechanism | Operate the on/off mechanism through repeated cycles and check that the magnet engages and releases as designed without sticking or visible damage. | Pass the agreed functional check for the specified model. Cycle count and operating-force limits should follow the product specification or buyer-supplier agreement. | Functional test procedure, model and lot identification, cycle results, and records of any adjustment or repair. |
| Dimensions and identification | Check key dimensions against the approved drawing using suitable measuring instruments. Confirm model, lot, and packaging identification against order documents. | Dimensions and identification should conform to the latest approved drawing and purchase requirements, including stated tolerances. | Dimension inspection report, drawing revision, instrument details, product traceability, and packing list. |
| ISO 9001:2015 quality management system | Review the current certificate and verify its status with the issuing certification body or applicable accreditation directory. | Check that the certificate is valid and that the certified organization, site, and scope are relevant to the manufacturing or supply activity. ISO 9001 certification concerns a quality management system; it is not, by itself, product certification or proof that a particular magnet passed testing. | Certificate number, issuing body, scope, covered site, validity dates, and verification result. |
| Pre-shipment quality documentation | Review the inspection package before shipment and confirm that reports correspond to the ordered model and production lot. | Documentation should be complete, traceable, and consistent with agreed drawings, specifications, and inspection requirements. | Final inspection report, pull-force results, surface inspection records, dimensional results, certificate verification, and lot traceability documents. |
Note: Pull-force ratings and inspection limits should be agreed for the specific magnet design and test conditions before production or purchase.
China’s Leading Shuttering Magnet Manufacturers: Products and Customization
China’s leading shuttering magnet manufacturers compete through product fit and customization, not merely holding-force claims. Options may include compact units for narrow beds, lever-release designs for quick repositioning, and housings matched to specific formwork dimensions. Custom orders can specify magnet layout, steel casing, release access, and compatible adapters. These details matter on a precast line: a lever that clears the mould edge can save awkward handling during changeovers. McKinsey Global Institute’s 2017 report, Reinventing Construction, estimated construction productivity growth at about 1% annually over two decades. Standardized tooling can support more repeatable work, though that figure does not measure magnet performance.
Tips: Share your mould drawings, steel thickness, and vibration conditions before ordering. Request test results for the stated holding force. A clean, flat contact surface matters; the magnet cannot compensate for a warped bed.
For supplier comparisons, ask how force was measured and whether the test reflects your actual steel plate. Thin steel, paint, gaps, and surface wear can reduce practical holding force. Request a sample for a production trial, then check positioning, release effort, and movement during vibration. Customization is useful, but more features are not always better. A small detail can still be missed: confirm that the lever remains accessible after concrete is placed. Keep drawings and inspection criteria consistent across repeat orders.
Comparing Suppliers Against the 24 kPa/m Hydrostatic Pressure Reference for Fresh Concrete
For shuttering magnet suppliers in China, the 24 kPa/m hydrostatic pressure reference offers a useful comparison point, not a universal pass-or-fail rating. Under this simplified model, pressure increases with concrete depth: a two-metre pour represents about 48 kPa at the base. Fresh concrete does not always behave like water, though. Mix design, temperature, pour speed, and vibration can change the pressure on the formwork.
A magnet’s stated holding force should be checked against the actual panel setup. Ask how it was tested, what steel plate thickness was used, and whether the figure describes pull-off force or resistance to sliding. These are different conditions. Paint, dust, uneven contact, and repeated handling can reduce real-world performance. Numbers need context. A supplier should explain how its test data relates to panel spacing and expected pressure, rather than presenting one force figure as proof of suitability.
A practical comparison includes drawings, test records, and a controlled site trial. Check magnet seating before the pour, then inspect for movement around joints and edges. A small gap matters. One easy mistake is comparing magnet ratings without considering the load carried by each unit. Even a careful calculation can miss site variation, so record the pour height and placement rate. The reference is useful, but it is not a substitute for checking the complete formwork system.
Get in touch with us,
We will contact you shortly!
What is the difference between Unline(Non-Epoxy Coated) or Lining(Epoxy Coated) Metal Drum?

Unline drums with internally bare metal surface is more susceptible to corrosion and rust while Lining drums are internally coated with Phenolic Epoxy Coating to provide a non-reactive barrier between the drum surface and your product, less risk of contamination. Note: Our Unline drums are coated with an anti-rust agent after washing to reduce risk of rust.
What are Unline(Non-Epoxy Coated) and Lining(Epoxy Coated) drums compatible with?

In Singapore, Recon Unline Drums are usually more costly than Recon Lining Drums. Hence, we recommend Recon Unline Drums to fill aromatics like Thinner, Xylene, Toulene& other solvents like Hexane, BA, CA, EA, MC, White spirit, etc.
We recommend the lower-priced Recon Lining Drums to fill hydrocarbons like IPA, Methanol, Ethanoland oil-based products like diesel, petrol, lubricants, engine, hydraulic, base, transmission fluid, additives, waste oil, etc.;
What is the difference between Grade A and Grade B Metal Drum ?

Grading of used drums are usually based on physical conditions like rustiness, deformities and residual contents. Grade A drums are totally free from internal rust, serious dents and are easy to clean. Grade B drums have different degrees of rust internally and aesthetically inferior compared to Grade A drums.
What content is suitable to fill in a Recon Grade A or Grade B Drum?

Recon Grade A drum is suitable to fill more costly virgin grade products while Recon Grade B drum is more suitable for recycled or waste products.
What is the difference between Open Top and Close Top Drums and their usage?

Closed top drums are for water and other liquid products. Open Top drums can be used for liquid too but are primarily for more viscous products. The Open Top (or open head with a lid) allows you to get in and out of the drum with your product easier.
What type of content are Metal or Plastic Drums suitable for?

Metal drums offer additional protection when dealing with potentially flammable substances. They provide superior fire resistance, impact protection, and longevity for storing class 1, 2, and 3 volatile chemicals.
Plastic HDPE Drums are suitable for corrosive chemicals like acids, alkaline and also water-based products.
Will there be any contamination in the reconditioned metal, plastic drums or IBC tanks?

All our reconditioned containers (metal/plastic drums, carboys, IBC tanks) are washed thoroughly with specially formulated cleaning agent, rinsed with clean water, dried, and tested for possible leakages during the recondition process. Stringent quality inspection is being conducted 100% on every reconditioned product before they are qualified for sale & delivery.
What is the drum gauge(thickness) and weight for reconditioned metal drums?

Reconditioned metal drums gauge can be 0.9mm to 1.0mm all round. Their weight can vary from 16 to 18kg.
Do you sell New Packaging Products too?

Yes, we are also a distributor for new pallets, metal drums, plastic drums, carboys, IBCs and stainless-steel tanks.
What additional services do you provide apart from selling reconditioned and new containers.?

We are an NEA licensed toxic industrial waste collector, who can collect and dispose of used toxic waste containers in Singapore.
Do you offer labelling and silkscreen on the containers ?

We can provide labelling and silk-screening on the containers.
Are you able to ship overseas ?

Yes, we can arrange export our products to any country in the world.
Leading the Way
to Carbon Neutrality