2026 Best Bucket Tooth Types for Global Buyers?
Choosing the right Bucket Tooth in 2026 will depend on ground conditions, machine size, and operating cost—not appearance alone. Global buyers now compare penetration, wear life, replacement speed, and total cost per operating hour.
Reports from Off-Highway Research, GlobalData, and Fortune Business Insights indicate continued demand for construction and mining equipment across Asia-Pacific, North America, Europe, and emerging markets. That growth increases the need for reliable wear parts. However, market forecasts often group bucket components within wider equipment categories. Their figures should guide decisions, not replace field testing.
Real experience matters. A tooth used in wet clay may perform poorly in abrasive granite. A sharp penetration tooth can reduce digging resistance, yet it may wear quickly in quarry work. Heavy-duty rock teeth offer stronger protection, but they can increase fuel use when the application does not require them.
As Caterpillar wear-parts specialist Edward D. O’Neil has stated, “The right tooth is selected by the application, not by size alone.” This principle remains practical for fleet managers and distributors. Still, buyers should verify the original source and wording before publishing any quotation.
The 2026 selection should examine standard, penetration, rock, abrasion-resistant, and side-cutter designs. Check alloy chemistry, casting quality, adapter fit, locking systems, and supplier traceability. Small mismatches create large costs.
There is no universal winner.
This guide compares leading Bucket Tooth types for global buyers. It considers productivity, service intervals, regional soil conditions, and realistic procurement risks. Some recommendations may change after site trials. That uncertainty deserves attention, because laboratory strength does not always equal longer service life in the field.
Define Bucket Tooth Types by Tip Profile, Adapter System, and Duty Class
2026 Best Bucket Tooth Types for Global Buyers?
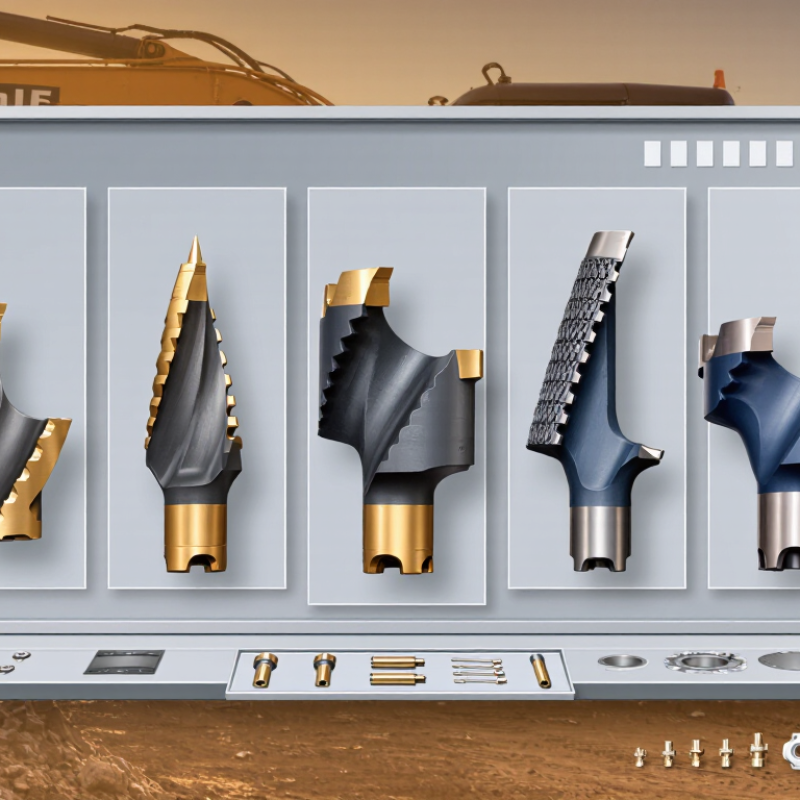
Bucket tooth selection starts with tip profile, not appearance.
A narrow, sharp tip penetrates compact clay and fractured rock with less initial resistance. A wider tip supports better material retention in sand, gravel, and general excavation. Twin-point profiles can improve breakout, but they may wear unevenly when operators force the bucket sideways. That detail is often missed.
Adapter systems define how the tooth transfers load.
Pin-on systems suit common excavators and simplify field replacement. A side-pin design can reduce access time in confined work areas. Weld-on adapters offer strong positioning, but replacement requires more fabrication skill. The wrong adapter can create pin movement, nose wear, and a loose tooth before the tip is fully consumed. It happens.
Duty class should match the material, cycle speed, and impact level.
The U.S. Geological Survey reported roughly one billion metric tons of construction sand and gravel production annually in recent estimates. That volume explains the demand for abrasion-resistant profiles. Meanwhile, Off-Highway Research has reported global construction equipment demand in the million-unit range, showing why standardized tooth inventories matter for international buyers.
A quarry handling crushed granite needs a heavier, reinforced tooth than a landscaping contractor moving topsoil. ASTM G65 abrasion testing can support steel comparison, but laboratory wear rarely matches every jobsite.
Buyers should record penetration time, tooth weight loss, and adapter damage across several shifts. The cheapest tip can become expensive when downtime is counted.
Match General-, Penetration-, Abrasion-, and Rock Teeth to Ground Conditions
For global buyers, bucket teeth should match ground conditions, not simply machine size.
General-duty teeth suit mixed soil, loose clay, and ordinary loading. Penetration teeth work better in compacted clay, frozen ground, and tightly packed material. Their narrower tips enter the face with less initial resistance. However, they can wear quickly in abrasive gravel.
USGS Mineral Commodity Summaries 2025 estimated U.S. crushed-stone production at about 1.5 billion metric tons in 2024. That scale highlights the importance of abrasion control. Abrasion teeth suit sand, gravel, and highly siliceous aggregate. They usually sacrifice some digging speed for longer wear life. World Mining Data 2025 also records sustained global mineral production, where bucket teeth often meet hard, fractured, and unpredictable faces. Rock teeth, with reinforced noses and stronger profiles, are safer choices for blasted rock and dense limestone.
Field inspection still matters more than a catalog chart. Look at tooth corner rounding, adapter movement, and the color of worn steel. A five-minute check can expose uneven loading. I have seen operators choose penetration teeth for rocky soil and lose the tips before the shift ended. That decision was understandable, but incomplete. Ground conditions change within one trench. Mixed tooth arrangements may improve performance, although they can complicate wear tracking. Buyers should compare tip geometry, alloy hardness, replacement access, and measured cost per cubic meter, not purchase price alone.
Compare 400–500 HB Wear Steel with ASTM A128 11–14% Mn Cast Teeth
2026 Best Bucket Tooth Types for Global Buyers?
Choosing between 400–500 HB wear steel and ASTM A128 cast teeth requires more than comparing hardness numbers. I have seen 400–500 HB components perform well in abrasive sand, gravel, and moderately compacted soil. Their consistent plate hardness supports predictable edge wear. However, excessive impact can cause cracking or premature tip deformation.
ASTM A128 teeth contain approximately 11–14% manganese and begin relatively soft. Under repeated impact, their surfaces work-harden while the core remains tough. This structure suits quarry rock, demolition debris, and heavily impacted digging conditions. They need impact to develop maximum wear resistance. Not always.
A hardness-only comparison can mislead buyers. A 450 HB tooth may outlast manganese steel in clean abrasion, but fail faster against large, sharp rocks. Manganese castings may resist impact better, yet suffer faster wear in low-impact sand. Tooth geometry, adapter fit, heat treatment, casting quality, and machine power also matter. Check chemistry reports, heat-treatment records, dimensional inspection, and hardness maps before ordering. Examine the pin bore and cutting edge, not only the certificate. One overlooked fit problem can waste more metal than a weaker alloy. Availability and replacement frequency also influence the real operating cost. The best choice depends on the bucket, ground conditions, and failure pattern recorded at the worksite.
2026 Best Bucket Tooth Types for Global Buyers? Compare 400–500 HB Wear Steel with ASTM A128 11–14% Mn Cast Teeth
Technical comparison for selecting excavator, loader, dragline and dredging bucket teeth
| Comparison Dimension | 400–500 HB Wear-Steel Teeth | ASTM A128 11–14% Mn Cast Teeth | Buyer Interpretation |
|---|---|---|---|
| Basic material form | Fabricated or machined tooth made from quenched-and-tempered abrasion-resistant plate or bar | Austenitic manganese steel casting covered by ASTM A128 | Fabricated teeth offer controlled geometry and machining flexibility; cast teeth allow complex tooth shapes and integrated features. |
| Nominal hardness at delivery | Approx. 400–500 HBW | Typically about 180–250 HBW | Initial hardness is not directly comparable: manganese steel is intentionally softer before work hardening. |
| Work-hardening capability | Limited to moderate | High under impact and compression | ASTM A128 manganese steel can develop a substantially harder surface in high-impact service, while retaining a tougher core. |
| Typical work-hardened surface | Usually remains near its supplied hardness, subject to wear, temperature and local deformation | Can commonly reach approximately 400–550 HB in heavily impacted zones; actual values depend on impact energy, deformation and test location | Work-hardening is application-dependent and should not be treated as a guaranteed uniform hardness value. |
| Typical tensile-strength range | Often approximately 1,250–1,600 MPa, depending on grade, thickness and heat treatment | ASTM A128 grades commonly provide tensile strength of at least about pega 800 MPa; exact values depend on the specified grade and casting quality | Use the material certificate for the exact grade and heat-treatment condition; published ranges vary by specification and producer. |
| Yield-strength behavior | Usually specified and relatively high for abrasion-resistant quenched-and-tempered steel | Generally not the primary selection criterion for ASTM A128; resistance increases after plastic deformation and work hardening | Wear-steel teeth provide more predictable initial strength; manganese teeth rely more on impact-induced strengthening. |
| Impact toughness | Good when the correct abrasion-resistant grade, thickness and heat treatment are selected | Very high in properly heat-treated condition | For severe impact, shock loading and large rock, manganese steel is often the safer starting point. |
| Abrasion resistance before work hardening | High | Moderate initially | 400–500 HB steel is advantageous where sliding abrasion dominates and impact is limited. |
| Best abrasion mechanism | Sliding abrasion, gouging abrasion and low-to-medium impact wear | Impact-abrasion combinations in which repeated loading produces surface hardening | Match the tooth material to the dominant wear mechanism rather than hardness alone. |
| Recommended operating conditions | Sand, gravel, clay, overburden, moderately abrasive soil and light-to-medium rock handling | Quarry rock, blasted rock, hard limestone, mineral handling and high-impact digging | Actual results depend on bucket design, tooth profile, machine power, ground conditions and operator technique. |
| Risk in severe impact | Higher risk of edge chipping, cracking or permanent deformation if the tooth is too hard or poorly supported | Lower fracture tendency when correctly heat-treated, but excessive deformation can occur under low-impact sliding wear | Do not select very hard steel solely for hardness when the application involves repeated shock loading. |
| Risk in low-impact sliding wear | Generally low | Potentially high before work hardening | In continuous abrasive sliding, a 400–500 HB material may retain its advantage over manganese steel. |
| Manufacturing flexibility | High: cutting, forming, welding and machining are possible with qualified procedures | Medium: near-net-shape casting is possible, but machining is more difficult and heat treatment is critical | Fabricated wear steel is useful for customized profiles and shorter production runs; cast manganese suits established casting patterns. |
| Repair and welding | Repair welding may be feasible with controlled preheat, low-hydrogen consumables and approved procedures | Welding is difficult because overheating can create brittle carbide precipitation; specialist procedures are required | Always use a qualified welding procedure and verify the specific material certificate before repair. |
| Dimensional consistency | Generally predictable after CNC machining and controlled fabrication | Dependent on pattern design, casting shrinkage, heat treatment and finishing allowance | Fabricated teeth may reduce fit-up variation; cast teeth can reduce part count and produce complex shapes. |
| Weight efficiency | Can be optimized through thinner sections and machined geometry, subject to structural design | Often requires robust sections to withstand deformation and casting-related design requirements | A lighter tooth may improve fuel efficiency, but structural safety and adapter compatibility remain essential. |
| Inspection priorities | Hardness mapping, plate or bar certification, weld quality, dimensional inspection and crack detection | Chemical composition, heat treatment, hardness, casting soundness, dimensional inspection and crack detection | For cast teeth, ultrasonic or radiographic inspection may be appropriate for critical applications. |
| Key chemistry consideration | Alloy design varies; verify carbon, chromium, nickel, molybdenum and boron where applicable | ASTM A128 commonly uses approximately 11–14% manganese with carbon controlled by the selected grade; exact chemistry must follow the specified grade | Request a heat or cast analysis rather than relying only on a generic “manganese steel” description. |
| Expected service-life pattern | More predictable from the beginning, with performance strongly linked to supplied hardness and tooth geometry | May improve after an initial running-in period as the working surface hardens under impact | Compare complete wear curves and replacement intervals, not only new-part hardness. |
| Best choice for global buyers | Choose for high abrasion and controlled impact | Choose for high impact with abrasive rock | The best material is application-specific; a site trial with identical tooth geometry is the most reliable validation method. |
Technical note: Hardness values are commonly reported as HBW, while some suppliers use “HB” as a general designation. ASTM A128 chemistry, mechanical properties and acceptance requirements vary by grade; confirm the applicable edition, grade, heat-treatment condition and inspection standard before purchasing. Actual tooth life also depends on adapter fit, tooth profile, bucket loading, ground conditions, impact energy and maintenance.
Verify Fit Through OEM Part Numbers, Pin Systems, and ISO 9001 Traceability
2026 Best Bucket Tooth Types for Global Buyers?
Selecting bucket teeth starts with the working ground, not appearance. General-purpose teeth suit mixed soil and loading work. Penetration teeth enter compact clay with a sharper profile. Abrasion-resistant teeth perform better in sand, gravel, and crushed rock. For severe rock, reinforced designs may reduce unexpected edge loss.
Verify the OEM part number before ordering. Match every digit, suffix, and revision. A similar-looking tooth can still fail during installation. Check the adapter shape, locking method, tooth opening, and pin diameter. Some systems use vertical pins, while others use horizontal pins or locking retainers. Measure the old parts directly. Photos alone can mislead. I have seen buyers confirm the tooth but overlook the adapter, causing costly delays. That mistake is easy to repeat.
Tips: Request a dimensional drawing and a fitment sheet. Confirm the tooth profile, material grade, heat-treatment record, and batch number. Ask for ISO 9001 traceability covering raw material, production, inspection, and shipment. Keep these records with the purchase order. A supplier may provide a certificate, but its scope should match the actual factory and product. Check it carefully. Also compare pin hardness and retainer quality, not only tooth price. A lower-cost tooth may wear faster in abrasive ground. Field conditions are rarely perfect, and laboratory data cannot predict every operator habit.
2026 Best Bucket Tooth Types for Global Buyers
Fit verification is strongest when buyers cross-check the OEM part number, pin-system details, dimensional requirements, and ISO 9001 traceability records. The chart shows the practical number of data fields commonly required for each purchasing checkpoint.
Rank 2026 Options by Wear Life, Fuel Demand, and Cost per Excavated m³
2026 Best Bucket Tooth Types for Global Buyers?
Rank 2026 Options by Wear Life, Fuel Demand, and Cost per Excavated m³
For abrasive granite, a heavy-duty abrasion tooth usually ranks first for wear life. Field records often show 300–900 working hours before replacement, depending on impact, moisture, and operator technique. It costs more upfront, yet fewer changes can reduce downtime. ASTM G65 abrasion testing helps compare alloys, but it cannot fully predict field performance. That limitation matters.
For mixed soil and weathered rock, a general-purpose tooth often gives the lowest cost per excavated m³. It cuts easily, needs moderate breakout force, and suits frequent material changes.
In lighter soil, a penetration tooth may improve bucket filling and reduce cycle resistance. However, its sharper profile can wear quickly in gravel. Small gains can disappear fast.
The U.S. Army Corps of Engineers’ 2024 equipment schedule models productive excavator fuel use at roughly 12–25 litres per hour for common 20–30-tonne classes. Tooth selection does not control fuel alone. Hydraulic condition, haul distance, loading depth, and idle time matter more. Buyers should divide hourly fuel cost, tooth cost, and maintenance cost by measured production. A 15% cheaper tooth is not automatically economical. This ranking is imperfect. Local material testing should challenge it.
Article Source:
Get in touch with us,
We will contact you shortly!
What is the difference between Unline(Non-Epoxy Coated) or Lining(Epoxy Coated) Metal Drum?

Unline drums with internally bare metal surface is more susceptible to corrosion and rust while Lining drums are internally coated with Phenolic Epoxy Coating to provide a non-reactive barrier between the drum surface and your product, less risk of contamination. Note: Our Unline drums are coated with an anti-rust agent after washing to reduce risk of rust.
What are Unline(Non-Epoxy Coated) and Lining(Epoxy Coated) drums compatible with?

In Singapore, Recon Unline Drums are usually more costly than Recon Lining Drums. Hence, we recommend Recon Unline Drums to fill aromatics like Thinner, Xylene, Toulene& other solvents like Hexane, BA, CA, EA, MC, White spirit, etc.
We recommend the lower-priced Recon Lining Drums to fill hydrocarbons like IPA, Methanol, Ethanoland oil-based products like diesel, petrol, lubricants, engine, hydraulic, base, transmission fluid, additives, waste oil, etc.;
What is the difference between Grade A and Grade B Metal Drum ?

Grading of used drums are usually based on physical conditions like rustiness, deformities and residual contents. Grade A drums are totally free from internal rust, serious dents and are easy to clean. Grade B drums have different degrees of rust internally and aesthetically inferior compared to Grade A drums.
What content is suitable to fill in a Recon Grade A or Grade B Drum?

Recon Grade A drum is suitable to fill more costly virgin grade products while Recon Grade B drum is more suitable for recycled or waste products.
What is the difference between Open Top and Close Top Drums and their usage?

Closed top drums are for water and other liquid products. Open Top drums can be used for liquid too but are primarily for more viscous products. The Open Top (or open head with a lid) allows you to get in and out of the drum with your product easier.
What type of content are Metal or Plastic Drums suitable for?

Metal drums offer additional protection when dealing with potentially flammable substances. They provide superior fire resistance, impact protection, and longevity for storing class 1, 2, and 3 volatile chemicals.
Plastic HDPE Drums are suitable for corrosive chemicals like acids, alkaline and also water-based products.
Will there be any contamination in the reconditioned metal, plastic drums or IBC tanks?

All our reconditioned containers (metal/plastic drums, carboys, IBC tanks) are washed thoroughly with specially formulated cleaning agent, rinsed with clean water, dried, and tested for possible leakages during the recondition process. Stringent quality inspection is being conducted 100% on every reconditioned product before they are qualified for sale & delivery.
What is the drum gauge(thickness) and weight for reconditioned metal drums?

Reconditioned metal drums gauge can be 0.9mm to 1.0mm all round. Their weight can vary from 16 to 18kg.
Do you sell New Packaging Products too?

Yes, we are also a distributor for new pallets, metal drums, plastic drums, carboys, IBCs and stainless-steel tanks.
What additional services do you provide apart from selling reconditioned and new containers.?

We are an NEA licensed toxic industrial waste collector, who can collect and dispose of used toxic waste containers in Singapore.
Do you offer labelling and silkscreen on the containers ?

We can provide labelling and silk-screening on the containers.
Are you able to ship overseas ?

Yes, we can arrange export our products to any country in the world.
Leading the Way
to Carbon Neutrality